


Low Pressure Moulding Tools
Application for automotive interiors
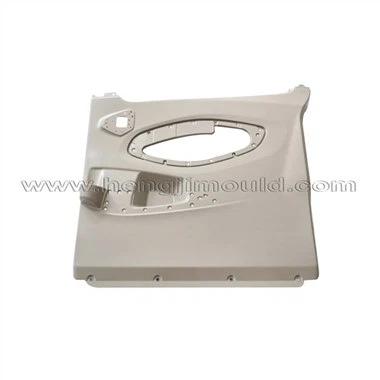
Low pressure moulding process makes products with a special surface layer of soft fabric which quite improves decoration and hand feeling. Normally components like map pocket framework, door panel garnish, ABC pillars,etc. are popularly required to make low pressure moulding tools.
Difference between low pressure injection and high pressure injection
|
Aspect |
Low Pressure Molding |
High Pressure Molding |
|
Pressure |
0.15-4MPa |
35-130MPa |
|
Temperature |
180~240°C |
230~300°C |
|
Mold Material |
Steel or Aluminium |
Steel |
|
Material |
Good Adhesion and Water-proof |
Bad Adhesion |
Advantages for Low Pressure Injection Molding (LPM)
(1) The goal of low-pressure injection molding is to bond the skin material with the plastic base material, eliminating the chance of peeling.
(2) The low pressure injection molding technique is more environmentally friendly since there is no glue application procedure required for the overmolding process.
(3) The internal structure of low-pressure double-layer injection molded components may be built freely, and the flexibility of surface modeling is larger than that of the overmolding technique, with clearer and more rigid modeling characteristics.
(4) Low-pressure injection molding eliminates the need for secondary cladding, increasing manufacturing efficiency.
(5) The handfeel and appearance of low-pressure injection molding items are excellent.
(6) Low pressure injection molding goods have a low injection pressure, which effectively protects the product's interior parts and has a low scrap rate.
Low Pressure Molded Product Design
(1) Part thickness design: surface layer material has a big influence to molten fluidity. Too thin causes short shot so to increase nozzles is necessary but tooling cost is also increased; Too thick increases material cost.
(2) Part edge design: after injection molding, there will be cover layer material remaining which needs post ultrasonic cutting or welding process. If the edge contour profile is too complicated, the production reject rate will go up.
(3) Part fracture surface design: in low pressure moulding tools, surface layer will be set smoothly and be pushed to the mould cavity by the core during mould close which bears stretching. Too deep part section will damage the cover so it should be double thought that the ratio of part surface radian to relative length should be smaller than that of elongation at break.
Notices for Low Pressure Moulding Tools
There should be submerged seal at mold moved side to prevent cover from slipping, the submerged seal and cut seal are determined by material type and thickness.
Cover fixing system
There is no structure movable for fixing of cover
Valve gate , product molded in core side and ejected at gate side.
The cover is plugged into mold cavity from upper of machine
Hot Tags: low pressure moulding tools, China low pressure moulding tools manufacturers, makers, low pressure injection polymer, low pressure injection assembly, low pressure injection painting, low pressure injection seminar, low pressure injection pressure, low pressure injection manufacturing
Previous
No InformationYou Might Also Like




Send Inquiry